Ti-1023 titanium rod properties and structure
Ti-1023 titanium alloy is a high reliability, low cost, high strength, high toughness, near beta titanium alloy. Its nominal composition is Ti-10V-2Fe-3Al. It has the advantages of high specific strength, good fracture toughness, large quenched section, small isotropic anomaly, low forging temperature, and strong stress corrosion resistance. It can meet the design requirements of high reliability and low manufacturing cost, so it is widely used in the aerospace field.
This article summarizes the reasonable production process of Ti-1023 alloy rods by investigating the composition of the ingots and the macroscopic, microstructure and mechanical properties of the rods, and achieves the expected results.
1. Experiment
In the experiment, 0A grade small particle sponge titanium and multi-element master alloy were fed together for 2 t, and melted three times in a vacuum consumable electric arc furnace to prepare a 650 mm Ti1023 titanium alloy ingot. The main component (mass fraction, %) V is 9.0%~11.0%. , Fe is 1.6%~2.2%, Al is 2.6%~3.4%, and the rest is Ti, which meets the requirements of GJB1538. After the steel ingot is cut into risers, bottoms, and saw blades, samples are taken from the axial circumferential head, middle, and tail (Figure 1) and the 9 o'clock position of the cross section (Figure 2), and the components are mainly tested using atomic emission spectrometry. Content of alloying elements (Al, V, Fe) and other impurity elements.

Figure 1 Schematic diagram of sampling points on the longitudinal surface of the ingot

Figure 2 Schematic diagram of sampling at the 9 o'clock position of the ingot cross section
Cut appropriate samples from Ti-1023 titanium alloy ingots, and use metallographic methods to determine the transformation temperature of αβ phase/β phase to be 805~810°C. The entire ingot is processed and forged using the "high-low-high-low" process route. A 45/50MN fast forging machine is used to open the steel billet in the single-phase area (β-phase area), and is finally forged into a 160mm finished bar.
According to the GJB1538 standard, 20mm thick specimens and 80mm long specimens were cut longitudinally from the 160mm bar, and various performance tests were conducted to determine the structure and mechanical properties of the Ti-1023 titanium alloy bar. After the 20 mm thick specimen is flattened, check the R state, β point (785℃×1.5 h WC 530℃×8 h AC) and solid solution aging (775℃×1.5 h WC 540℃×8 h AC). Magnify the tissue, use the ICX41M metallographic microscope to observe the tissue morphology and take metallographic photos. After the 80 mm long sample rod was heat treated at 775°C × 1.5 h WC and 540°C × 8 h AC in a muffle furnace, the H-5550K semi-automatic band saw was used to cut the transverse and longitudinal specimen blanks at D. /4 sample block. , processed into mechanical property test specimens according to standard requirements, and subjected to room temperature tensile mechanical property tests. Tensile tests were measured on a CMT5205 tensile testing machine. At the same time, the finished bars also undergo contact ultrasonic non-destructive testing.
2 Results and analysis
2.1. Analysis of chemical composition of steel ingots
According to the product sampling requirements, samples were taken at 9 points on the longitudinal head, middle, tail and cross section of the steel ingot surface to detect the content of main alloy elements in different parts. The test results show that the chemical composition of the tablet meets the requirements of relevant technical standards. In particular, the detection results of the content of impurity elements (C, N, O, H) at the head and tail positions of the longitudinal surface all meet the standard range requirements, indicating that the purity of the ingot is very high.
Figure 3 is a statistical chart of the chemical composition of the main alloy elements in different parts of the ingot. The sampling point locations are the longitudinal surfaces of the outer round head, middle and tail of the ingot (points 1 to 3), and the three cross sections of the head, middle and tail (points 4 to 30). As can be seen from Figure 3, the chemical compositions of the main elements Al, V, and Fe measured at the upper, middle, and lower points on the outer circular surface fluctuate slightly. The Al element content is 3.16%~3.24%; the V element content is 9.86%. ~10.06%; Fe element content is 1.77%~1.89%; Al and V element deviation is not more than 0.2%, among which the deviation of easily segregated element Fe is not more than 0.12%, indicating that the axial chemical composition of the produced ingot is uniform; ingot The nine-point chemical composition test on the head, middle and bottom sections all meets the standard requirements. The maximum deviation of the main elements Al and V is not more than 0.13%~0.27%, and the deviation of the easily segregated Fe element is not more than 0.34%. Overall, the ingot has good uniformity and all elemental components meet technical standards.

Figure 3 Alloy element composition diagram at different positions of Ti-1023 titanium alloy ingot
During the vacuum consumable arc melting process of steel ingots, there is Fe, an element that is prone to segregation, and uneven composition or segregation may occur during the melting of steel ingots. According to the titanium alloy phase diagram and alloy solidification theory, under normal solidification conditions, alloy elements with segregation coefficient k ≥ 1 are not prone to segregation, unless the alloy elements and the mother alloy are not completely homogenized during the smelting process; alloys with segregation coefficient k < 1 Elements, even if the alloy is homogeneous in the molten state, there is still a certain difference between the solid phase composition and the liquid phase composition at the same temperature during solidification. The element content in the liquid phase is always higher than that in the solid phase, causing the ingot to easily segregate in the middle and head. As can be seen from Figure 3, the Fe element content is slightly higher at the center point of the head of the section, followed by the middle, and finally the tail, which is consistent with the above analysis.
Overall, the chemical composition of the main alloy elements of the Ti-1023 titanium alloy 2t grade ingot is evenly distributed and of good purity, all of which meet the technical requirements of the ingot. This also illustrates the importance of raw material selection and ingot casting in the smelting process. Process control and other aspects are reasonable and feasible.
2.2. Bar structure and morphology analysis
Photos of the forged state (R state) of Ti-1023 titanium alloy after cutting the specimen from the head and tail position of the 160mm rod for surface corrosion.
As can be seen from Figure 4, the low-magnification structure of the bar is uniform fuzzy crystal, and there are no metallurgical defects such as segregation and inclusions, indicating that the forging blank has achieved sufficient deformation. Utilizing the large tonnage pressure of the 4,500-ton fast forging machine, the "high-low-high-low" process route is used for multiple fire forgings to fully break the as-cast grains, reverse forging of the billet, and improve the forging penetration of the billet. characteristics, making the structure of the rod more uniform. The forging process takes advantage of the processing characteristics of very slow grain growth when the beta matrix recrystallization of the near-beta alloy is completed quickly, causing the metal grains to repeatedly break, the sub-grains to merge and grow, and the grain boundaries to migrate, so that the final bar structure tends to be uniform. , which lays a good foundation for the uniform structure and good performance of the rod.

Figure 4 R-state photos of φ160mmTi-1023 titanium alloy rod at different positions: (a) head; (b) tail
Cut transverse samples from different areas (edge, D/4, center) corresponding to the position of the spindle head on the bar test piece, and observe the R state and microstructure after solution aging heat treatment. , see Figure 5 and Figure 6. As can be seen from Figure 5, the R-state microstructure of the rod consists of a β matrix and uniform, fine, equiaxed primary α phases distributed on the matrix. The average size of the primary α phase is about 3.5 μm, and the volume fraction of the primary α phase is more than 35%. It can be seen from Figure 6 that after solid solution aging treatment, the equiaxed grains are more obvious, indicating that the process parameters such as forging deformation are reasonable.
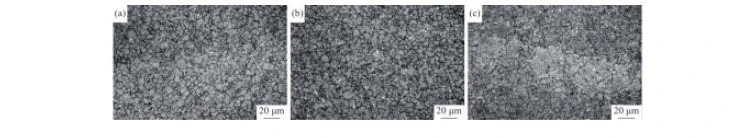
Figure 5 R-state microstructure of φ160mmTi-1023 titanium alloy rod at different positions: (a) edge; (a) edge; (b) D/4; (c) center

Figure 6 Microstructure of Φ160mmTi-1023 titanium alloy rod at different locations after solution aging treatment: (a) edge; (a) edge; (b) D/4; (c) center
2.3. Bar β point detection results
The equilibrium distribution constant of Fe element in Ti-1023 titanium alloy is 0.3, which has a great tendency to segregate. The main reason for the formation of β points in Ti-1023 titanium alloy is the local segregation and enrichment of "Fe" alloy materials, which results in the β phase transformation temperature of this part being lower than that of the matrix, thus forming a phase that does not contain primary α phase or the content of α phase is relatively sparse. The rich Fe area. The β point will seriously affect the plasticity and low-cycle fatigue life of the alloy.
The uneven Fe composition of TB6 alloy ingots is the "innate" factor that leads to the formation of β spots, while the subsequent heat treatment and heat treatment process are the "acquired" factors that affect the formation of β spots. According to the heat treatment process in GJB1538, 785 ℃ × 1.5 h WC and 530 ℃ × 8 h AC were selected to prepare rods. Observation of the rod body revealed that there was no local abnormality in the macroscopic morphology of the rod body (Figure 7); the primary α phase content in the microstructure was about 15%, which met the GJB1538 standard requirement of the primary α phase content being greater than 10%. As shown in Figure 8. This shows that the smelting process and forging process have a certain significant effect on controlling β spots.

Figure 8 Microstructure of Φ160mm Ti-1023 titanium alloy rod: (a) edge; (b) D/4; (c) center
It can be clearly seen from Table 1 that all properties of the rod meet the requirements of relevant indicators. It has high plasticity, uniform transverse and longitudinal strength, and a certain margin compared to the standard value in plasticity. It shows that appropriate technology is used during forging to achieve relatively sufficient deformation, so that the structural uniformity of the bar in all directions is relatively good and the difference is small.
2.5. Ultrasonic testing of bars
SonATEST 380M ultrasonic flaw detector and Olympus V109 probe were used to conduct ultrasonic flaw detection on Φ160 mm Ti-1023 titanium alloy finished rods. Judging from the waveform, the noise level is not higher than 20%, the noise is uniform, and there are no obvious defect signals. , the change amplitude of the bottom wave is less than 6 dB, and the noise level is half of the sound path? 1.2 –9 dB ~ –12 dB (Figure 9), indicating that the finished rod can meet the A1 level requirements of the GB/T5193-2007 standard. In Figure 9, the abscissa represents depth, and the ordinate represents signal height. Full screen is calculated as 100%.